Gear Module vs Diametral Pitch: A Buyer's Guide
Gear module and diametral pitch describe tooth size using different measurement conventions. For values defined in the same reference plane, module in millimeters equals 25.4 divided by diametral pitch in teeth per inch. Use that conversion to interpret a specification, then verify pressure angle, tooth count, reference plane, profile modifications, and mating geometry before approving a replacement.
1. Understand what the two numbers describe
1.1 Read module as diameter per tooth
For a spur gear, module is the reference diameter in millimeters divided by the tooth count. A larger module therefore represents larger tooth spacing at the reference circle. KHK's gear module explanation describes this relationship and compares module with other pitch conventions.
1.2 Read diametral pitch as teeth per diameter
Diametral pitch, commonly abbreviated DP, is the tooth count divided by the reference diameter in inches. A larger DP represents finer teeth, which is the opposite numerical trend from module. The diameter in this definition is the reference diameter, not the distance measured over the tooth tips.
1.3 Keep pitch separate from overall part size
Two gears can share a module while having different diameters because their tooth counts differ. Likewise, two gears can have similar outside diameters while using incompatible tooth pitches. Read the pitch value together with the tooth count and gear family rather than using it as a complete size designation.
2. Convert module and diametral pitch correctly
2.1 Use the reciprocal relationship
The conversion follows directly from the two definitions and the relationship of 25.4 millimeters to one inch. Divide 25.4 by DP to obtain module, or divide 25.4 by module to obtain DP. Use corresponding reference planes when applying the relationship to helical gearing.
DP = 25.4 / m
m: module in mm; DP: diametral pitch in teeth per inch.
2.2 Label the units in a calculation sheet
A spreadsheet should show the input designation, input units, conversion, and resulting designation. For a helical gear, it should also identify normal or transverse values. Keeping those labels beside the numbers makes it easier to detect a reversed formula or a reference-plane error during review.
2.3 Preserve the controlling designation
Keep the original drawing requirement as the controlling value unless engineering approves a change. Show a converted value as reference information when that is its intended purpose. This prevents a rounded display value from silently becoming a new manufacturing requirement on a later purchase order.
3. Use a conversion table without rounding away the design
3.1 Check representative conversions
The following values are calculated from m = 25.4 / DP. Rounded entries are marked with an approximation symbol and are intended for comparison. The table is not a list of ABEJA stock sizes, available tooling, or approved substitutes.
| Controlling input | Equivalent value | Interpretation |
|---|---|---|
| Module 1 | 25.4 DP | Exact numerical conversion |
| Module 1.5 | ≈ 16.933333 DP | Retain the module requirement |
| Module 2 | 12.7 DP | Different from 12 DP |
| Module 2.5 | 10.16 DP | Different from 10 DP |
| 8 DP | Module 3.175 | Exact numerical conversion |
| 12 DP | Module ≈ 2.116667 | Retain the DP requirement |
| 20 DP | Module 1.27 | Different from module 1.25 |
| 24 DP | Module ≈ 1.058333 | Different from module 1 |
3.2 Distinguish conversion from substitution
Writing module 1.27 as the equivalent of 20 DP expresses the same tooth-size value in a different system. Replacing it with module 1.25 changes that value. The second action is a design substitution and requires a review of the mating geometry and installed arrangement.
3.3 Do not infer availability from a neat number
An exact conversion can produce a value that differs from a supplier's preferred tooling or product series. Ask the supplier to distinguish the requested specification from any proposed alternative. Commercial convenience does not establish that the alternative will mesh with the retained gear.
4. Separate reference, outside, and working diameters
4.1 Use the reference diameter for pitch
Reference diameter is a geometric value used to define the tooth system. For a spur gear, d = mz, where z is the tooth count. It is not normally a physical cylindrical surface that can be identified simply by placing calipers across the finished gear.
4.2 Apply the outside-diameter formula only to its case
For the standard unshifted external spur geometry discussed here, outside diameter is da = m(z + 2). That relationship assumes the standard addendum of one module. KHK's gear dimension reference separates this case from profile-shifted and other gear geometries.
4.3 Recognize when working diameter differs
The working pitch circles describe the installed pair's operating geometry. They can differ from the reference circles when the pair operates at a modified center distance. Keep reference and working dimensions clearly labeled so a correct measurement is not inserted into the wrong formula.
5. Work through a standard spur gear example
5.1 Define the hypothetical component
Consider a standard unshifted external spur gear with module 2 and 40 teeth. Its reference diameter is 2 × 40 = 80 mm, and its standard outside diameter is 2 × 42 = 84 mm. These values illustrate geometry only and do not establish load capacity, material, accuracy, or a finished production specification.
5.2 Describe the same pitch in inch terms
The equivalent diametral pitch is 25.4 / 2 = 12.7 DP. The reference diameter is 40 / 12.7 ≈ 3.149606 inches, which converts back to 80 mm. Both calculations describe the same reference geometry when the remaining tooth requirements are unchanged.
5.3 Identify what is still missing
The example does not define the pressure angle, face width, bore, or mating component. It also leaves material condition, tooth tolerances, and acceptance requirements open. ABEJA's spur gear project guidance connects those missing fields to a usable component and assembly specification.
6. Connect pitch with tooth count and center distance
6.1 Keep the speed ratio separate
For a simple external gear pair, the tooth-count ratio determines the speed-ratio magnitude. Module determines the size scale of the teeth and reference circles. Changing module while retaining both tooth counts changes the dimensions but does not by itself change that tooth-count ratio.
6.2 Calculate a standard center distance
For an unshifted standard external spur pair, center distance is a = m(z1 + z2) / 2. A module 2 pair with 40 and 80 teeth therefore has a standard center distance of 120 mm. Use the appropriate pair calculation when profile shift or a different operating center distance is specified.
6.3 Check fixed housing constraints early
A retained housing usually makes shaft spacing a major constraint. Provide its controlled center-distance dimension and relevant tolerances during the geometry review. Do not ask a supplier to choose a nearby pitch value without explaining which mating parts and installation dimensions must remain fixed.
7. See why module 2 and 12 DP are different
7.1 Compare the reference diameters
A 40-tooth module 2 spur gear has an 80 mm reference diameter. A 40-tooth 12 DP spur gear has a reference diameter of 40 / 12 inches, or approximately 84.667 mm. Matching tooth counts therefore do not make these two specifications dimensionally equivalent.
7.2 Compare the complete pair
A standard 40/80-tooth pair at 12 DP has a center distance of 5 inches, or 127 mm. The module 2 version requires the 120 mm standard center distance calculated above. This 7 mm difference illustrates why rounding module ≈ 2.116667 down to module 2 is a redesign rather than a conversion.
7.3 Reject an unsupported mixed-pitch replacement
Moving the shafts does not turn mismatched tooth pitches into an equivalent approved pair. Review any proposed geometry change with the retained mate and the required operating conditions. If a supplier proposes replacing both gears, evaluate the new pair and its interfaces as a complete alternative.
8. Verify pressure angle as a separate requirement
8.1 Read the pressure-angle field explicitly
A pitch match alone does not establish a compatible involute mesh. Pressure angle is a separate part of the tooth definition and must be reviewed with the mating gear. Never assume a familiar value merely because the tooth count and module appear ordinary.
8.2 Name the plane on a helical drawing
Helical gears can be specified using normal or transverse pressure angle. Equal numerical values in those different planes do not describe the same geometry when the helix angle is nonzero. Keep the pressure-angle label aligned with the drawing's module or DP reference system.
8.3 Resolve missing information before manufacture
An old part number or a photograph may not reveal the original pressure angle. Ask for the mating drawing, manufacturer data, or a suitable geometry inspection when the requirement is unknown. Record the confirmed result in the released drawing instead of carrying a verbal assumption into production.
9. Distinguish normal and transverse module
9.1 Locate the two reference planes
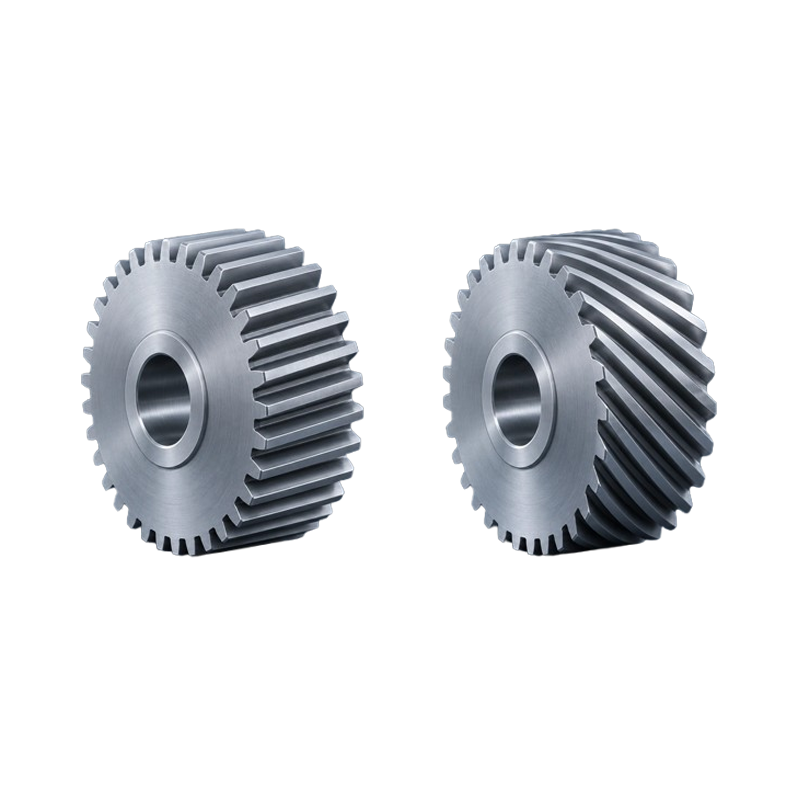
The transverse plane is perpendicular to the shaft axis, while the normal plane is perpendicular to the tooth trace. In a spur gear these pitch directions coincide. A helical gear's inclined tooth trace makes the distinction necessary, as explained in KHK's transverse module reference.
9.2 Relate the values through the helix angle
For a helical gear, transverse module equals normal module divided by the cosine of the reference helix angle. Use mt = mn / cos β and d = mtz to obtain the reference diameter. Label β as the reference-cylinder helix angle and use a consistent angular unit in the calculation.
9.3 Convert DP within the same plane
Apply mn = 25.4 / DPn for normal values and mt = 25.4 / DPt for transverse values. A normal DP converted directly into an unlabeled module can conceal the plane information needed to calculate diameter. Preserve the subscript or write the plane in full wherever the value appears.
10. Calculate a helical example step by step
10.1 Begin with clearly labeled inputs
Consider a hypothetical helical gear with normal module 2, 40 teeth, and a 20° reference helix angle. Its transverse module is 2 / cos 20° ≈ 2.128356. The normal module remains 2; the different transverse value comes from the reference-plane relationship.
10.2 Calculate the diameter and both DP values
The reference diameter is approximately 2.128356 × 40 = 85.134 mm. Normal DP is 25.4 / 2 = 12.7, while transverse DP is approximately 11.934096. Rounding is shown for readability and should not replace the controlling input values in a released specification.
10.3 Compare it with a transverse-module design
A different 40-tooth helical gear specified at transverse module 2 would have an 80 mm reference diameter. That is not the same gear as the normal-module example, despite both carrying the number 2. ABEJA's helical gear specification page identifies reference plane, helix hand, and mating information as inputs to the pair review.
11. Allow for profile shift and tooth modifications
11.1 Do not recover module from every outside diameter
The shortcut m = da / (z + 2) follows from the standard unshifted spur outside-diameter formula. It can give the wrong conclusion when the gear has profile shift, altered addendum, tip reduction, or a different tooth system. Use it as a conditional screening calculation only when those assumptions are justified.
11.2 Preserve the modification information
Record any specified profile-shift coefficient and the reference system used for it. Keep approved tooth modifications and inspection requirements connected to the same drawing revision. A replacement defined only by module and tooth count can lose a feature that was intentional in the original design.
11.3 Distinguish design geometry from wear
A used gear's tooth surfaces may no longer represent its original geometry. Damaged tips or worn flanks can also make simple dimensional estimates misleading. Identify the part's condition and compare available drawing or inspection evidence before using it as the sole manufacturing reference.
12. Investigate an unidentified replacement gear
12.1 Collect the information that is available
Record tooth count, visible markings, outside dimensions, face width, bore details, and the shaft arrangement. Include photographs with an identifiable scale and views of the mating component. Label measured values as observations so they are not confused with approved nominal dimensions and tolerances.
12.2 Escalate uncertain tooth geometry to inspection
Module, pressure angle, profile shift, and wear can be difficult to separate using a few workshop measurements. Ask a qualified gear specialist to define the inspection needed to resolve those uncertainties. Keep the original part, mate, and housing information available until the replacement geometry is agreed.
12.3 Define whether the mate can change
Replacing one member of an existing pair imposes different constraints from replacing both members. State which components must remain and whether their condition has been assessed. If the gear family itself is uncertain, the guide to gear types and shaft layouts can help frame the initial discussion.
13. Write a tooth specification that survives purchasing
13.1 Group the geometry fields together
Place the pitch designation, tooth count, pressure angle, and gear-family information in one controlled drawing table. Add normal or transverse labels, helix angle, and hand when applicable. Reference the mate and assembly drawing so a reviewer can check the tooth definition in its intended context.
| Field | Information to record | Common ambiguity to resolve |
|---|---|---|
| Gear form | Spur or helical; external or internal; shaft arrangement | Applying an external spur formula to another family |
| Pitch designation | Module or DP; exact controlling value; units | Rounded equivalent treated as a substitute |
| Reference plane | Normal or transverse where applicable | The same number assigned to different planes |
| Tooth geometry | Tooth count; pressure angle; helix angle and hand | Pitch match assumed to establish all compatibility |
| Modifications | Profile shift; specified tooth modifications | Outside diameter treated as proof of standard geometry |
| Installed pair | Mate revision; center distance; backlash conditions | Part inspection mistaken for assembly acceptance |
13.2 Label converted dimensions as reference values
If both unit systems appear, state which designation controls and how secondary values are rounded. Check that software exports preserve those labels and the intended precision. A drawing that gives two conflicting nominal requirements can produce a quotation dispute even when each individual conversion looks plausible.
13.3 Add the non-geometry purchasing requirements
The pitch table does not replace the material, treatment, quantity, or acceptance specification. Add those fields before requesting a firm manufacturing quotation. The custom gear RFQ checklist provides a broader structure for completing the order package.
14. Review supplier alternatives without losing compatibility
14.1 Require a clear description of the change
Ask the supplier to state whether an alternative changes only the notation or changes actual tooth geometry. A unit conversion and a different available cutter size are separate proposals. Record the original requirement and proposed value side by side before assessing price or delivery implications.
14.2 Recheck the mesh and its clearances
If geometry changes, review the mate, center distance, interference, and required backlash under the proposed arrangement. KHK's backlash guidance shows why tooth thickness and mounting conditions cannot be reduced to a pitch label. Include the applicable operating conditions in the engineering approval.
14.3 Release one agreed definition
Document the accepted alternative in the drawing or an approved deviation that the purchase order references. Identify any changes to the mating parts or inspection requirements at the same time. This gives later repeat orders a clear baseline instead of leaving compatibility dependent on an old email exchange.
15. Use a final pitch verification checklist
15.1 Complete the geometry checks before release
The checklist below is an original review aid for engineering and purchasing. Use it to confirm that a converted pitch value has not hidden an unresolved design decision. Assign an owner to any missing item and keep its status visible in the release record.
- Identify the controlling pitch designation and its units.
- Confirm normal or transverse reference plane where required.
- Recalculate the conversion without rounding the controlling input.
- Verify tooth count, pressure angle, helix angle, and helix hand.
- Separate reference, outside, and working diameters.
- Confirm profile shift and any specified tooth modifications.
- Review the retained mate, installed center distance, and backlash requirements.
- Approve any substitution and update the controlled documentation.
15.2 Keep the evidence with the part record
Save the source drawing, calculation, supplier clarification, and approval against the same part revision. For a replacement developed from a sample, include the inspection basis and any unresolved limitations. The next buyer should be able to understand why the selected pitch is correct without repeating the investigation.
15.3 Request a specification review from ABEJA
Use ABEJA Gears' inquiry page to share the gear and mating information available for your project. Identify whether you need a quote against an approved drawing or help resolving an incomplete specification. Confirm the available engineering, manufacturing, and inspection scope in the written response.
16. Frequently asked questions
16.1 Is module 2 the same as 12 DP?
No, module 2 is equivalent to 12.7 DP in the same reference plane. A 12 DP gear corresponds to module approximately 2.116667. Treating those two values as interchangeable changes the tooth pitch and requires a design review.
16.2 Can I identify module from outside diameter?
Outside diameter and tooth count can support an estimate when the part is known to be a standard unshifted external spur gear. The relationship is not a universal identification method for modified, helical, damaged, or worn gears. Confirm the tooth geometry from controlled data or appropriate inspection before approving manufacture.
16.3 Does converting DP to module make a gear compatible?
An exact conversion changes how the pitch is expressed, not the physical gear. Compatibility still depends on the remaining tooth geometry, mating component, and installed conditions. Keep the reference plane and all other requirements intact when presenting a specification in another unit system.
Related Posts
Rack and Pinion Sizing: An OEM Selection Guide
Gear Backlash: How to Specify and Measure It
Gear Module vs Diametral Pitch: A Buyer’s Guide
One Response